
Advanced Honing Navigator │ Choose the Ideal Honing Machine » Honing in India » Honing Machines in Gurugram
Honing Machines in Gurugram
Regional guide · Gurugram–Manesar
Honing machines in Gurugram: what local vehicle production demands from bore finishing
Gurugram and Manesar sit in Haryana, which the state's own Economic Survey calls the largest automobile hub in India. Most local honing work finishes bores in engine, transmission, brake and hydraulic parts made for nearby two-wheeler and car plants. This guide links the region's production data to the parts that need honing, the machine configurations that suit them and the checks to make before buying.
Key takeaways
- Most honing around Gurugram is high-volume automotive component finishing, so cycle time and size stability usually matter more than maximum bore range when choosing a machine.
- The part sets the configuration: small precision bores, long bores and heat-treated gear bores each call for different tooling, sizing and loading.
- Vehicle capacity is growing at Kharkhoda and in neighbouring states, so new lines should allow for relocation and changeover, not only today's part.
- Before ordering, run test honing on the actual workpiece and get the India service scope in writing.
Why honing demand clusters around Gurugram and Manesar
Maruti Suzuki, Honda and Hero MotoCorp all build vehicles in Gurugram or Manesar, and their component suppliers follow the NH-48 corridor from Gurugram through Manesar towards Dharuhera. Every engine, gearbox, brake system and hydraulic unit built for these plants contains bores that must hold size, form and surface texture.
Production indicators behind local honing demand
| Indicator | Figure | What it means for bore finishing |
|---|---|---|
| Maruti Suzuki production, FY2025-26 | 23.4 lakh vehicles (2.34 million), a company record, from plants in Gurugram, Manesar, Kharkhoda and Hansalpur | Engine and transmission parts for these volumes are finished in steady, repeat production runs |
| Maruti Suzuki installed capacity, May 2026 | 26.5 lakh vehicles a year across Gurugram, Manesar, Kharkhoda and Hansalpur | New capacity creates new supplier lines, not only extra shifts on existing machines |
| Honda Motorcycle & Scooter India, Manesar | First plant, opened May 2001; capacity of 1.6 million units on 52 acres | Two-wheeler engines add cylinder, connecting-rod and small valve bores to local demand |
| Hero MotoCorp, Haryana | Manufacturing plants in Gurugram and Dharuhera, among its Indian sites | Two large two-wheeler supply chains draw on the same regional supplier base |
| India vehicle wholesales, FY2025-26 | 46.4 lakh passenger vehicles and 2.17 crore two-wheelers, both records | National demand is still rising, which supports continued investment in component lines |
| India auto component turnover, FY2025-26 | ₹7.59 lakh crore (USD 85.9 billion), up 12.7% year on year | Much of the bore finishing happens at component suppliers, so their investment drives machine demand alongside the OEM plants |
| Japanese business establishments in Haryana | 601 as of October 2024 | Japanese-affiliated companies make up a sizeable share of the regional customer base for machine builders |
Company figures cover all listed plants unless a single site is named. National figures are shown for scale and are not Gurugram-only totals; no current official count of Gurugram district factories is published in a comparable form.
References: Economic Survey of Haryana 2025-26 · Maruti Suzuki FY2025-26 production · Maruti Suzuki Kharkhoda plant 2 · HMSI factories · Hero MotoCorp BRSR FY2024-25 · SIAM FY2025-26 wholesales · ACMA FY2025-26 review · Embassy of Japan and JETRO list of Japanese business establishments
Components made in the region that typically need honing
Honing follows boring or reaming and brings a bore to its final size, roundness, straightness, cylindricity and surface texture. Parts go to honing when the drawing specifies form or texture that boring alone cannot hold consistently.
Common honed parts in the Gurugram supply chain
| Component | Why the bore is honed | What buyers usually specify |
|---|---|---|
| Cylinder bores and liners | A crosshatch pattern holds oil for the piston rings, and bore geometry controls ring sealing and oil consumption | Size, cylindricity, crosshatch angle, roughness profile |
| Connecting rods | Big-end and small-end bores must match bearing shells and piston pins closely | Size, roundness, bore-to-bore parallelism |
| Gears and pinions | Heat treatment distorts the bore, and honing restores the fit on the shaft | Size after hardening, roundness, surface finish |
| Hydraulic valve bodies and spools | Small running clearances decide leakage and response | Size tolerance in microns, cylindricity, matched clearance |
| Brake master cylinders and caliper bores | Seals must slide without leaking along the full stroke | Size, straightness, roughness in the seal zone |
Published results show the precision range involved: one Japanese machine builder reports a 0.7 μm roundness and 1.5 μm cylindricity on a φ18 mm sintered connecting rod. Results like this apply to that part and set-up only; confirm your own target through test honing.
References: Sunnen: honing after boring · NISSIN processing examples
Choosing a honing machine configuration for local production
A tier-1 line shipping to an OEM every day and a job shop handling mixed batches need different machines. Start from the production pattern, then check that the bore range fits.
High-volume tier-1 line
- Vertical machines with single or multiple spindles, sized to the takt time of the customer line.
- In-process or post-process gauging that corrects size automatically as honing stones wear.
- Rough and finish honing in one machine when the cycle allows it.
- Automatic loading so size control does not depend on one operator.
Job shop or mixed low-volume work
- Manual or semi-automatic machines with a wide diameter range and quick tool changes.
- Horizontal machines for long bores such as hydraulic cylinder tubes.
- Simple fixtures that can be swapped between part families.
- Operators trained to read bore gauges and adjust the stroke and stone feed.
Configuration decisions and what drives them
| Decision | Options | Choose based on |
|---|---|---|
| Machine orientation | Vertical or horizontal | Bore length, part weight and floor space |
| Number of spindles | Single or multi-spindle | Monthly volume, target cycle time and part mix |
| Sizing method | Manual gauging, post-process feedback or in-process air gauging | Tolerance band and how often the line can stop for checks |
| Stone expansion | Mechanical, hydraulic or servo-controlled | How finely stock removal must be controlled near final size |
| Loading | Manual, gantry or robot | Shift pattern, labour availability and cycle-time target |
Device capabilities and manufacturer support requirements vary from business to business, differing for precision components, large components and heavy industry, and component repair and processing.
We have carefully selected the honing machines that are best suited to companies based on the features and challenges of their varied businesses, freeing them from needing to rely on specific operators. Please use the information on this site in your comparisons and deliberations.
How the regional supply base is shifting
Vehicle capacity is moving beyond Gurugram and Manesar. A honing machine bought today may need to move, change part families or serve a customer in another state within its working life.
What is changing
- Haryana allotted Maruti Suzuki 800 acres at IMT Kharkhoda in Sonipat district. Production began in February 2025, and a second plant took Kharkhoda to 5 lakh vehicles a year in May 2026.
- JETRO's India head has said high land prices and rising labour costs are steering new Japanese investors from Haryana towards Uttar Pradesh and Rajasthan.
- Battery-electric vehicles have no engine cylinder bores, but they still use gears, brake hydraulics and motor housings.
What to plan for
- Ask whether the machine can be moved and recommissioned if the line relocates towards Kharkhoda or across the state border.
- Check tooling changeover time if engine-bore volumes fall and gear or hydraulic parts replace them.
- Confirm that service engineers cover every plant you supply, not only a Gurugram address.
How quickly electrification reduces engine-bore work depends on each customer's product plan. Treat it as a question for your OEM customers rather than a fixed forecast.
References: Economic Survey of Haryana 2025-26 · Maruti Suzuki Kharkhoda plant 2 · JETRO India head on Haryana land prices
Sourcing routes in Gurugram: listings, local offices and imports
Search results for honing machines in Gurugram are dominated by B2B listings. Listings speed up price discovery, but the service arrangement behind the machine matters more once the machine is running in production.
Buying routes compared
| Route | Works well when | Confirm first |
|---|---|---|
| B2B listings and local dealers | You need quick quotes for standard or manual machines | Who builds the machine, who installs it and where spares come from |
| Machine builder's India office | The part needs test honing, matched tooling or line automation | Which work is done in India and which goes back to the factory abroad |
| Direct import | A customer specifies a machine or process already approved elsewhere | Lead time, import costs and remote support hours |
| Used or refurbished machine | Capital is tight and tolerances are within the machine's proven range | Spindle and stroke condition, gauging system and controller parts |
Some overseas builders keep a contact in Gurugram. NISSIN ProSOL, for example, lists an India branch office in Gurugram and reports more than 100 honing machines delivered to India since the 1990s.
Operators matter as much as the machine. Honing machine operator vacancies in Gurugram and Manesar appear in the same search results as machine suppliers, so ask what operator training is included and how long it lasts.
Service questions to ask any supplier
- Which repairs can engineers based in India complete, and what is the target response time for your plant?
- Which honing stones, tools and spare parts are stocked in India?
- What do installation, commissioning and operator training include?
- How are warranty claims, annual maintenance contracts and factory escalation handled?
Reference: NISSIN ProSOL India support information
What to prepare before test honing or a quotation
Suppliers can only propose a configuration and cycle time when they know the part and the result it must reach. Send these details with the enquiry.
- Part drawing, bore geometry and datum definition
- Material, heat treatment and hardness
- Incoming bore size, stock allowance and variation from the previous operation
- Final size tolerance, form requirements and surface texture, with the measurement method
- Monthly volume, target cycle time and shift pattern
- Loading method, automation scope and available floor space
- Power supply, coolant conditions and inspection records required by your customer
If a requirement is still open, label it as open. This stops a provisional assumption in the quotation from being read as an agreed machine capability.
Frequently asked questions
Is honing needed if boring already brings the bore to size?
Boring sets bore position and size, and honing brings roundness, cylindricity and surface texture within tighter limits. Honing is needed when the drawing specifies form or texture that boring cannot hold consistently in production.
Can one honing machine handle both two-wheeler and car parts?
Often it can, if every bore falls within the machine's diameter and length range and the fixtures can be changed quickly. Compare changeover time with your batch sizes before relying on one machine for both.
Is a used honing machine a safe choice in Gurugram?
It can work for manual or low-volume jobs. Check the stroke mechanism, spindle condition, gauging system and whether controller parts are still available before you pay.
Do honing machine suppliers in Gurugram offer test honing?
Some do, but where the test runs varies. Ask whether samples are honed in India or at the builder's factory abroad, how long results take and which measurement method is used.
[Advertisement]
Top Three Honing Machines
That Free You from Reliance on Individual Operators
Top Three Honing Machines
That Free You from Reliance on Individual Operators
BS-VI standards and growing EV demand are driving unprecedented needs for precision machining.
While the "overseas components + local assembly" model keeps initial costs low, design mismatches and unclear accountability create long-term risks.
Integrated management from design to assembly ensures consistent machining accuracy regardless of operator, minimizing material loss, accelerating ROI, and building the foundation for global trust.
Advertiser Disclosure:
We receive compensation from some of the companies listed below.This compensation may affect which companies are included and the order in which they appear.
For
precision component suppliers
precision component suppliers
G Series
NISSIN ProSOL
NISSIN ProSOL
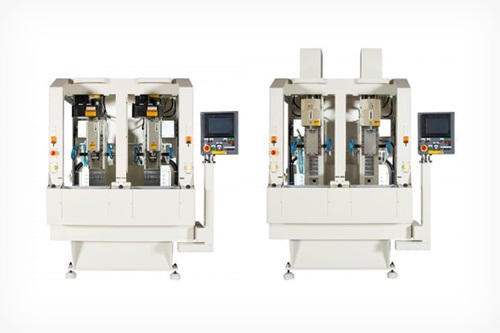
Source: NISSIN ProSOL official website https://mktg.nissin-mfg.co.jp/product/gseries/
This honing machine synchronizes stroke and stone expansion in 0.01 μm increments, enabling precision honing of holes as small as 3 mm in diameter and 80 mm deep, even in hard materials.
Automatic electronic control and made-to-order jigs reproduce the techniques of veteran operators.
These honing machines eliminate deviations in the manufacturing of precision components such as control valves while also reducing personnel costs.
| Bore Diameter |
⌀3~⌀100 |
|---|---|
| Workpiece Length |
130mm |
| Spindle Stroke Length |
Max. 300mm |
Main Applications
Gears / Connecting rods / Hydraulic valves, etc.
For
large components and heavy industry
large components and heavy industry
VL Series
Nagel
Nagel
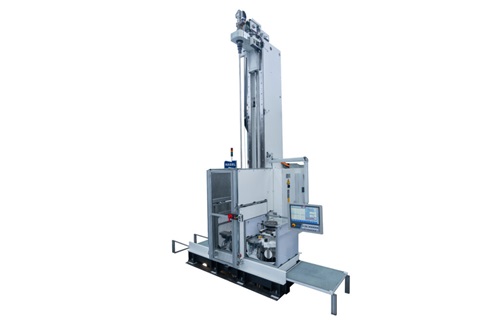
Source: Nagel official website https://nagel.com/en/products/honing/honing-machines/tube/
Machine height can be reduced through pit installation, reducing the footprint and using less volumetric space. It also makes it easy to mount and unmounts heavy objects such as engine blocks, reducing the operation workload.
They can even cut the large machining allowances unique to heavy industry in short amounts of time.
| Bore Diameter |
~⌀350 |
|---|---|
| Workpiece Length |
3,800mm |
| Spindle Stroke Length |
Not specified on official website |
Main Applications
Long pipes and tubes / Piston rods / Heavy workpieces / Exterior diameter processing, etc.
For
parts repairs and processing-on-consignment
parts repairs and processing-on-consignment
SV Series
Sunnen
Sunnen
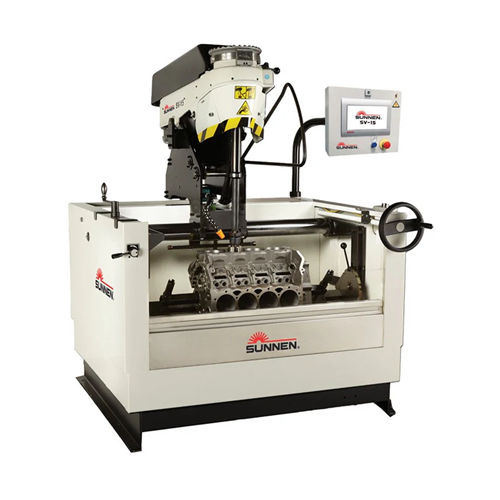
Source: Sunnen official website https://sunnen.com/products/sv-15-vertical-honing-machine
A graph showing the status of the hole being honed is displayed on-screen, in real time. This makes it easy to visually understand where the workpiece is and how it is warped, accelerating repair decisions.
These systems can store up to 100 processing settings at any time. They can also be backed up via USB, so even for small-lot, high-mix jobs, you can instantly reproduce the same processing as in previous jobs. They also shorten set-up times.
| Bore Diameter |
~⌀203 |
|---|---|
| Workpiece Length |
279mm |
| Spindle Stroke Length |
~225mm |
Main Applications
Engine blocks, etc.